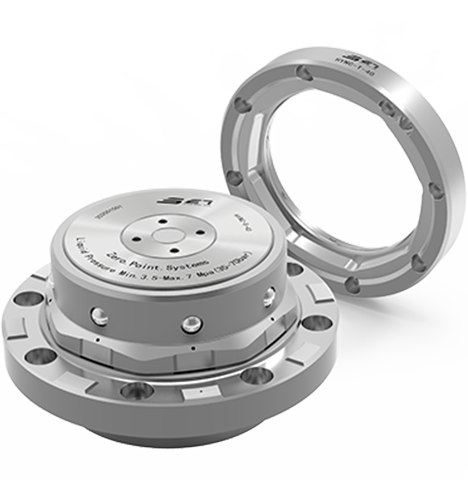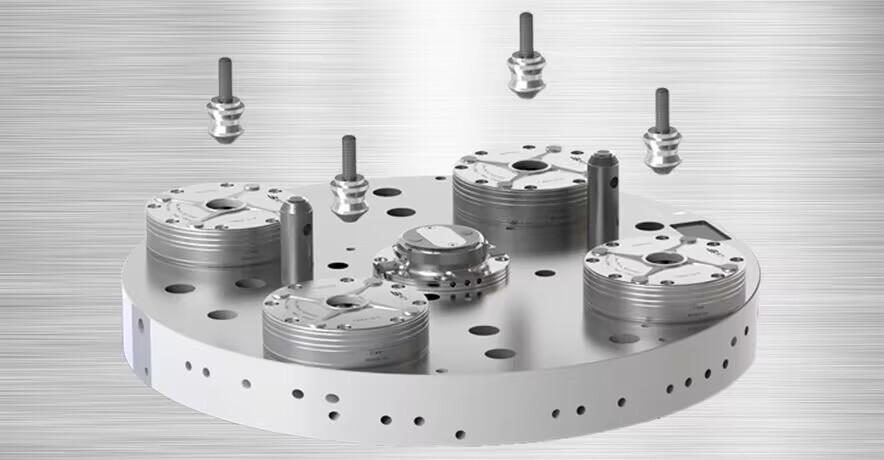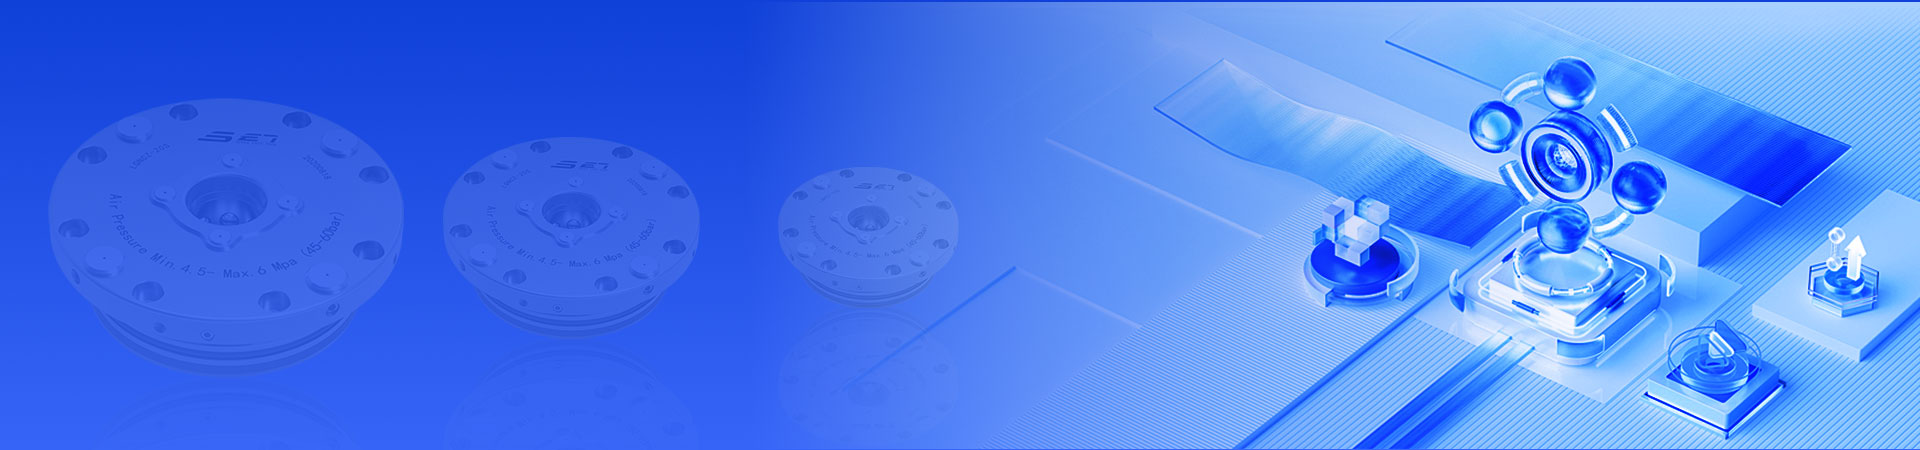
Octagonal conical zero positioner can be unlocked by air pressure and mechanically locked by spring.
Repeated positioning accuracy <0.003mm, a single locator clamping force 8kN, air pressure 0.6MPa, lifting force 1kN.
Eight-sided constraint, suitable for single use.
With clamping detection interface, positioning surface cleaning function.
Hardened stainless steel, temperature range 0℃~70℃. It is suitable for automation, lathe, CNC, four-axis machining and the occasions with high requirements for centering accuracy, axial force and centrifugal force.
Pneumatic/hydraulic/mechanical unlock, spring lock;
Repeated positioning accuracy <0.003mm;
Eight-sided constraint, suitable for single use;
Material: hardened stainless steel;
With clamping detection interface;
With positioning surface cleaning function.


| Model number | Pressure pattern | Hydraulic type | |||||||
|---|---|---|---|---|---|---|---|---|---|
| HQNC-10 | HQNC-20 | HQNC-40 | HQNC-60 | HYNC-10 | HYNC-20 | HYNC-40 | HYNC-60 | ||
| Clamping force (kN) | 3.5 | 5 | 8 | 15 | 10 | 16 | 25 | 40 | |
| Lifting Force | Atmospheric pressure 0.6MPa(kN) | 0.5 | 0.5 | 1 | 1.5 | / | |||
|
Hydraulic pressure 3.5MPa(kN) |
/ | 1.5 | 3.2 | 4.6 | 4.5 | ||||
| Hydraulic pressure5MPa(kN) | / | 5.7 | 9.8 | 15.3 | 20.1 | ||||
| Hydraulic pressure7MPa(kN) | / | 11.4 | 18.7 | 29.4 | 40.9 | ||||
| Allowable eccentricity when pallet clamping(mm) | ±1 | ±1 | ±1 | ±1.5 | ±1 | ±1 | ±1 | ±1.5 | |
| Lift (pallet lift when relaxed)(mm) | 0.3mm | ||||||||
| Operating ambient temperature(℃) | 0~70℃ | ||||||||
| Weight | The main clamp(kg) | 1.8 | 3.4 | 6.8 | 12 | 1.8 | 3.4 | 6.8 | 12 |
| Tray adapter(kg) | 0.4 | 0.8 | 1.6 | 3 | 0.4 | 0.8 | 1.6 | 3 | |
Outline dimensions
Main calmping apparatus
| Order number | ØDN | ØD1 | ØD2 | ØD3 | ØD4 | ØD5 | H | HA | HB | HC |
|
HQNC-S-10 HYNC-S-10 |
100 | 97 | 89 | 70 | 60 | 74 | 55 | 21 | 12 | 21 |
|
HQNC-S-20 HYNC-S-20 |
125 | 121 | 111 | 86 | 75 | 89 | 71.5 | 29 | 15 | 21 |
|
HQNC-S-40 HYNC-S-40 |
160 | 156 | 140 | 110 | 95 | 110 | 82 | 38 | 19 | 24 |
|
HQNC-S-60 HYNC-S-60 |
200 | 194 | 178 | 142 | 115 | 130 | 92.5 | 41 | 23 | 25 |
| Order number | HF | ØQA | ØQB | ØQC | MA | MB | MC |
ØRA (H7) |
ØRX (±0.01) |
ØRY (±0.01) |
|
HQNC-S-10 HYNC-S-10 |
4.4 | 9.5 | 5.5 | 5.5 | M6*1 | 89 | R43.5 | 5 | 38 | 25 |
|
HQNC-S-20 HYNC-S-20 |
4.4 | 11 | 6.5 | 6.8 | M8*1.25 | 110 | R55 | 6 | 47 | 31 |
|
HQNC-S-40 HYNC-S-40 |
4.4 | 14 | 7 | 8.5 | M10*1.5 | 140 | R67 | 8 | 60 | 39 |
|
HQNC-S-60 HYNC-S-60 |
4.4 | 17.5 | 11 | 11 | M12*1.75 | 175 | R81.5 | 10 | 77 | 49 |
Tray adapter
| Order number | ØD1 | ØD2 | ØD3 | ØD4 | ØD5 | H | H1 | H2 |
|
HQNC-T-10 HYNC-T-10 |
100 | 82 | 70.3 | 89 | 97 | 21 | 7.5 | 15 |
|
HQNC-T-20 HYNC-T-20 |
125 | 100 | 86.3 | 111 | 121 | 26 | 10 | 19 |
|
HQNC-T-40 HYNC-T-40 |
160 | 125 | 110.3 | 140 | 156 | 29 | 12 | 22 |
|
HQNC-T-60 HYNC-T-60 |
200 | 166 | 142.3 | 178 | 194 | 35 | 15 | 28 |
| Order number | A | ØG | ØN | M | ØT |
ØRA (H7) |
ØRX (±0.01) |
ØRY (±0.01) |
|
HQNC-T-10 HYNC-T-10 |
90 | 4.5 | 4.5 | M5*0.8 | 8 | 5 | 38 | 25 |
|
HQNC-T-20 HYNC-T-20 |
113 | 5.5 | 5.5 | M6*1 | 9.5 | 6 | 47 | 31 |
|
HQNC-T-40 HYNC-T-40 |
143 | 6.8 | 6.8 | M8*1.25 | 11 | 8 | 60 | 39 |
|
HQNC-T-60 HYNC-T-60 |
180 | 9 | 9 | M10*1.5 | 14 | 10 | 77 | 49 |
Mounting dimension drawing
Main calmping apparatus
| Order number | ØD1 | ØD2 | A | B | H | H1 | M | ØN | ØU | TA | ØTB |
ØRA (H7) |
ØRX (±0.01) |
ØRY (±0.01) |
|
HQNC-S-10 HYNC-S-10 |
74 | 73.7 | 89 | 90 | 28 | 11 | M5 | 2.5 | 3 | R43.5 | 5 | 5 | 38 | 25 |
|
HQNC-S-20 HYNC-S-20 |
89 | 88.7 | 110 | 115 | 30 | 11 | M6 | 2.5 | 3 | R55 | 5 | 6 | 47 | 31 |
|
HQNC-S-40 HYNC-S-40 |
110 | 109.9 | 140 | 146 | 32 | 13 | M8 | 5 | 4 | R67 | 10 | 8 | 60 | 39 |
|
HQNC-S-60 HYNC-S-60 |
130 | 129.7 | 175 | 186 | 37 | 13 | M10 | 5 | 4 | R81.5 | 10 | 10 | 77 | 79 |
Tray adapter
| Order number |
ØDN (H6) |
ØA | B | C | H1 | ØN |
ØRA (H7) |
ØRX (±0.01) |
ØRY (±0.01) |
|
HQNC-T-10 HYNC-T-10 |
82 | 5.5 | 90 | M4 | 10 | 50 | 5 | 38 | 25 |
|
HQNC-T-20 HYNC-T-20 |
100 | 6.8 | 113 | M5 | 14 | 65 | 6 | 47 | 31 |
|
HQNC-T-40 HYNC-T-40 |
125 | 9 | 143 | M6 | 17 | 80 | 8 | 60 | 39 |
|
HQNC-T-60 HYNC-T-60 |
166 | 11 | 180 | M8 | 17 | 120 | 10 | 77 | 49 |
A short-cone ball lock zero-point positioning system uses a short-cone locating interface combined with a ball-lock clamping mechanism to position and secure compatible fixtures or pallets. The system is designed for repeatable CNC workholding and quick fixture changeover.
The short-cone locating interface establishes the positioning reference between the zero-point receiver and the compatible fixture or pallet. The ball-lock mechanism secures the interface, while the pneumatic system can be used to release the clamping mechanism during fixture changeover.
Yes. The compact locating interface and repeatable positioning concept make the system suitable for selected 5-axis machining and multi-axis workholding applications. The final configuration should be selected according to the machine, fixture geometry and machining requirements.
This configuration uses pneumatic actuation for releasing the clamping mechanism. The exact operating pressure, clamping force and installation requirements depend on the selected model and technical specification.
The applicable SET configuration can provide repeatability up to 0.005 mm. Actual performance depends on the product model, installation accuracy, locating interface, fixture condition and machining environment. Please refer to the specific product drawing for the exact specification.
Yes. The zero-point interface can be integrated with compatible custom fixtures, pallets and workholding plates. Fixture dimensions, locating interface, pull studs and clamping requirements should be confirmed before production.
Yes. The pneumatic configuration can be integrated into automated fixture and pallet changeover systems. Additional sensors, air connections, robotic interfaces or control components may be required depending on the automation design.
Selection depends on the required positioning accuracy, clamping force, fixture size, workpiece weight, machine-table configuration, installation method and automation requirements. SET can recommend a suitable configuration after reviewing the machine and fixture information.
Yes. SET is a manufacturer specializing in zero-point positioning systems, zero-point clamping systems, gripping systems, clamping systems and customized tooling solutions for CNC machining and industrial automation.
Yes. SET provides customized zero-point positioning and workholding solutions according to machine-table dimensions, fixture requirements, workpiece size, positioning accuracy, clamping force and automation conditions.
Yes. Technical drawings, product specifications and configuration information can be provided for applicable products. Customers can contact SET with their machine model, fixture dimensions and application requirements to confirm the correct configuration.
SET can support customized industrial workholding and tooling projects. OEM or non-standard requirements should be evaluated according to the technical specifications, application conditions and production requirements of the project.
For a zero-point positioning system quotation, provide the CNC machine type, machine-table dimensions, fixture or pallet dimensions, workpiece weight, required positioning repeatability, clamping requirements, pneumatic conditions and automation requirements. Drawings or photos are also helpful for technical evaluation.
If you are interested in our products, please consult us